Winlog Evo - SCADA HMI Software

Winlog Evo - SCADA HMI Software
Visualizzazione post con etichetta hardening. Mostra tutti i post

venerdì 14 settembre 2018

Supervisory control of an automatic installation for heat treating

Winlog SCADA HMI Software, MQTT/Modbus IoT Gateway
The system manages a continuous line for carburizing, tempering, hardening heat treatments. The SCADA application communicates with a PLC Siemens SIMATIC S7 network using MPI protocol (server Applicom).

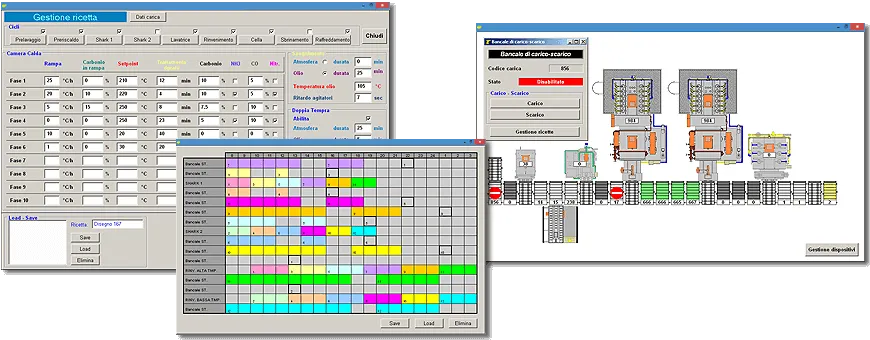
Batch materials are linked to their treatment recipes and positioned on parking platforms. An asynchronous process logic verifies furnaces and washers availability to receive the materials. The system allows accessing the recipes database that contains batch identification and process data. The main template shows position and progress status of each process and provides a detailed view of each heat treatment element.

At the end of any batch production, the application generates quality control reports containing batch identification data and temperature and carbon percentage charts for each phase of the treatment; in each report it is available a section in which it is possible to insert the measure of mechanical characteristics of produced material.

Optionally, Sielco Sistemi offers a scheduling and optimizing batch system that allows sending of many consecutive recipes to the treatment line and obtaining the best sequence to use all the heat treatment elements in a rational and economic way.


mercoledì 12 settembre 2018

Quality control in metal heat treatment

Winlog SCADA HMI Software, MQTT/Modbus IoT Gateway
The system has been designed to ensure the quality control for heat treatments in a plant division equipped with heterogeneous furnaces (multi-chamber furnaces, pit furnaces, tempering and hardening furnaces), replacing traditional paper recorders and creating production report.

Furnaces are equipped with their own instrumentation (PLCs, Eroelectronic/Gefran controllers, recorders) and can perform different kind of heat treatments (hardening, tempering, annealing, stabilization, normalization). The system gathers heat treatments measures of all division from a parallel data acquisition network without entering any interference to the existing control instrumentation; collected data (temperatures, carbon percentages) are continuously referred to theoretical curves values set in every production recipe to verify the quality of the process.

At the end of every production process, reports are generated containing load identification data, process variable curves and alarms. All historical data and reports are exported in a Microsoft Office compliant format and extended to the quality control division.

Alarms coming from process and machines are recorded and broadcast to maintenance staff and, in case of not guarded plant, to surveillance staff.

Two PClog client stations and a PClog server TCP/IP provide system HMI, ensure data integrity and maintain plant work continuity. This system is well suited in those cases where it is important to have global vision of several process executed by several machines without local HMI.